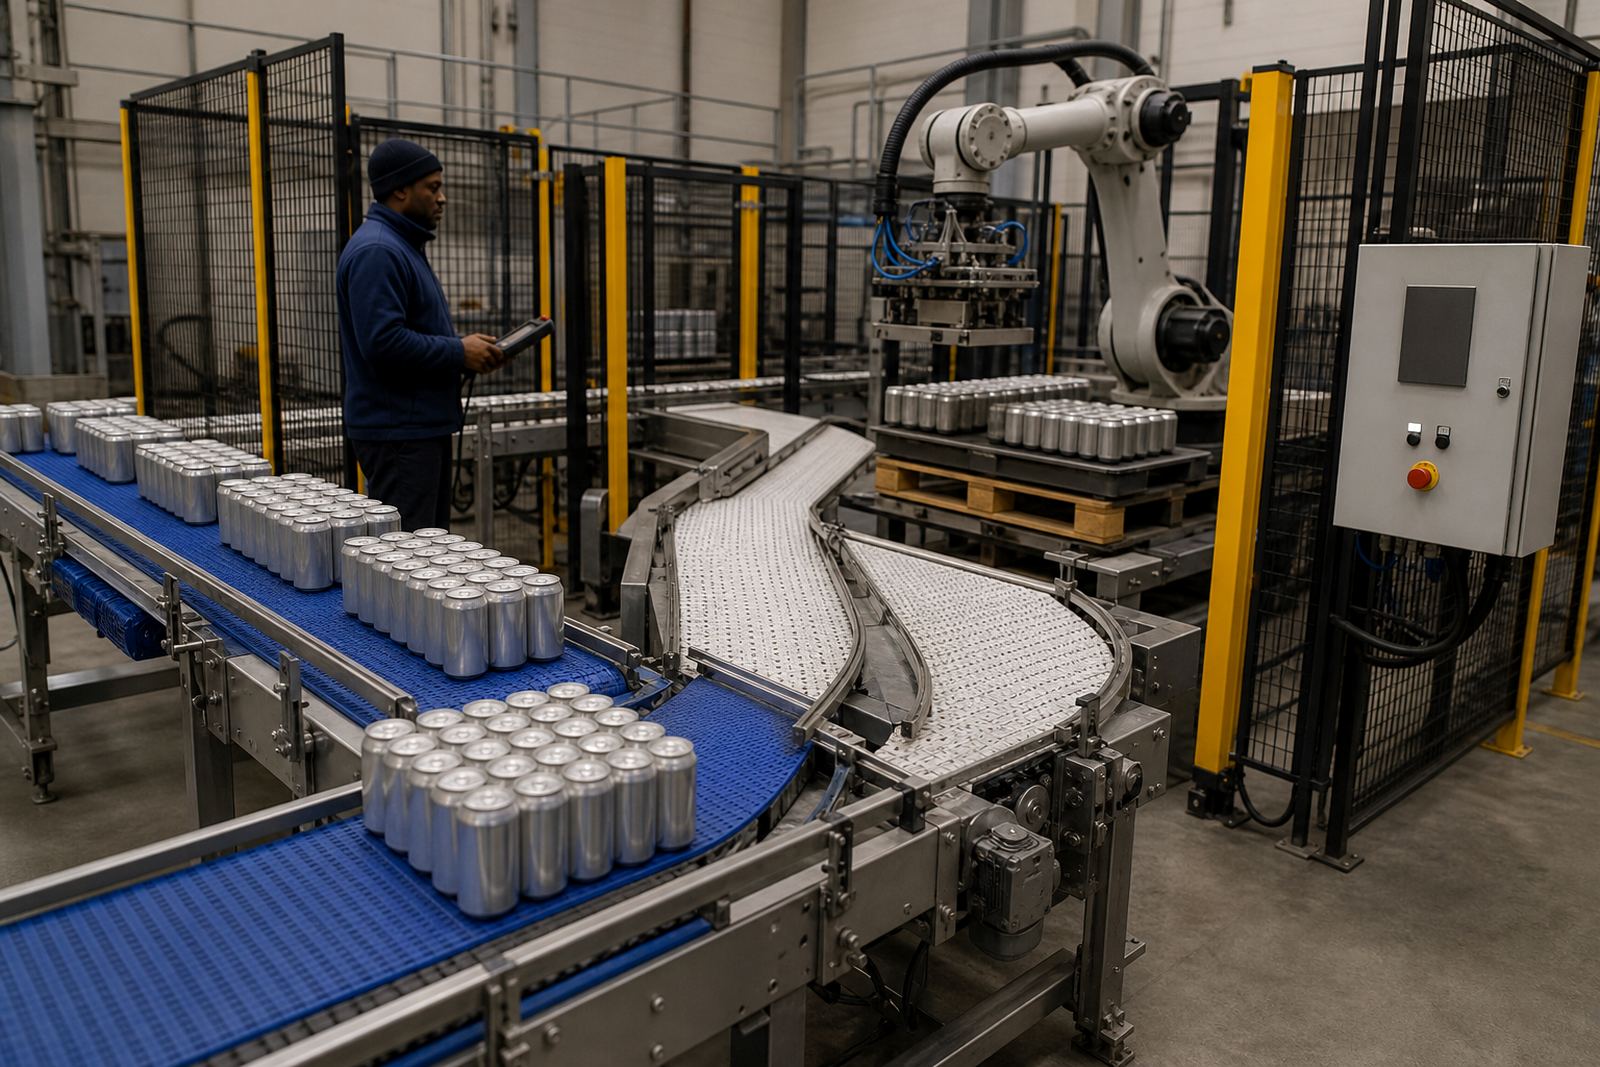
Mixed SKU Line In Midrand Needs A Better Fit
The site was a Midrand manufacturer working with a wide mix of carton sizes, case weights and pallet build requirements across more than one product family. The old arrangement relied too heavily on manual packing and a fixed pallet pattern, which meant every changeover cost time and added pressure on the team during peak shifts.
The brief was clear: keep the existing conveyor route where possible, reduce manual handling and make the palletising side flexible enough for regular pattern changes.
- Site: Midrand, Gauteng
- Application: mixed carton packing and palletising retrofit
- Line type: existing conveyors with manual intervention points
- Changeover need: frequent pallet pattern updates for multiple SKUs
What The Site Needed Before Any Equipment Was Ordered
We started with a site line survey and a practical walk through of the infeed, carton accumulation, pallet build area and the transfer points between them. That showed where cartons were backing up, where operators were doing unnecessary lifting and where the line could be reworked without moving major plant. The team also needed safe access around the robot zone, because the packing area sat close to pedestrian routes and the forklift aisle.
Before any mechanical changes were locked in, we completed risk assessment support and mapped the line around the real operating conditions. That included guarding positions, emergency stops, access gates and the need to keep maintenance access clear. Each site needs its own risk assessment, because one factory's layout and traffic flow can be very different to another even if the process sounds similar.
- Existing conveyor heights and transfer points checked on site
- Operator access and changeover points marked out
- Guarding footprint planned around maintenance access
- Control panel location reviewed for daily use and fault finding
Retrofit Scope: Packing, Palletising And Controls
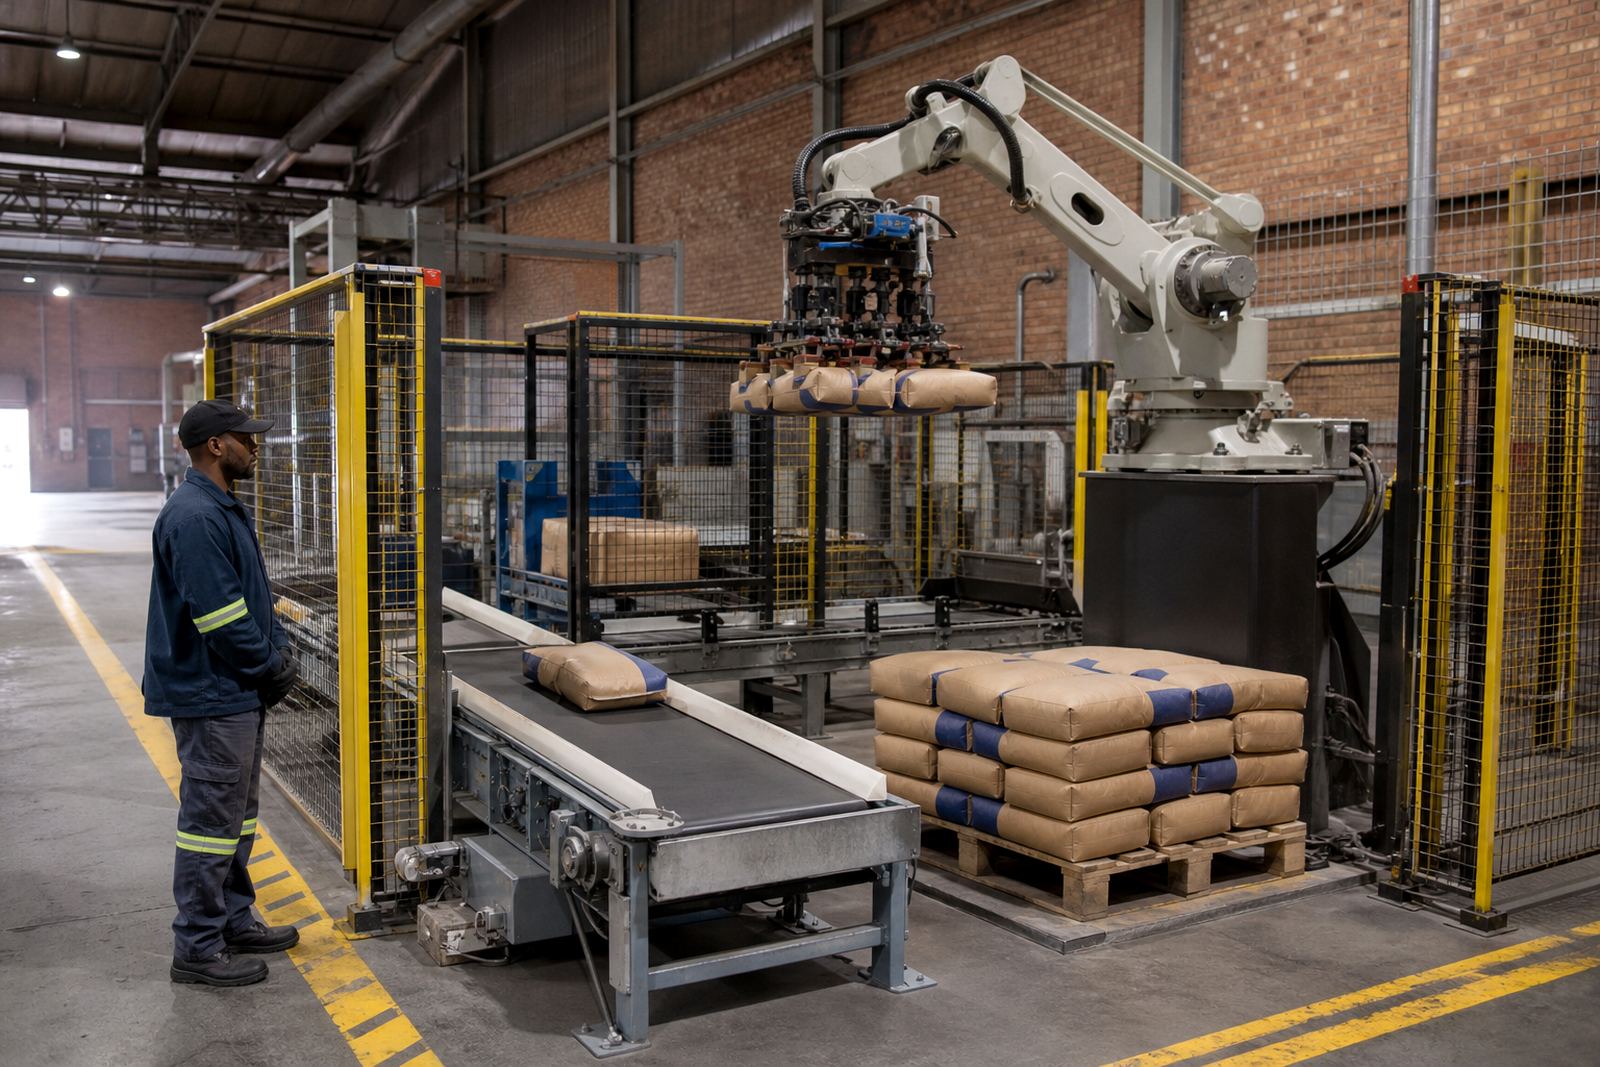
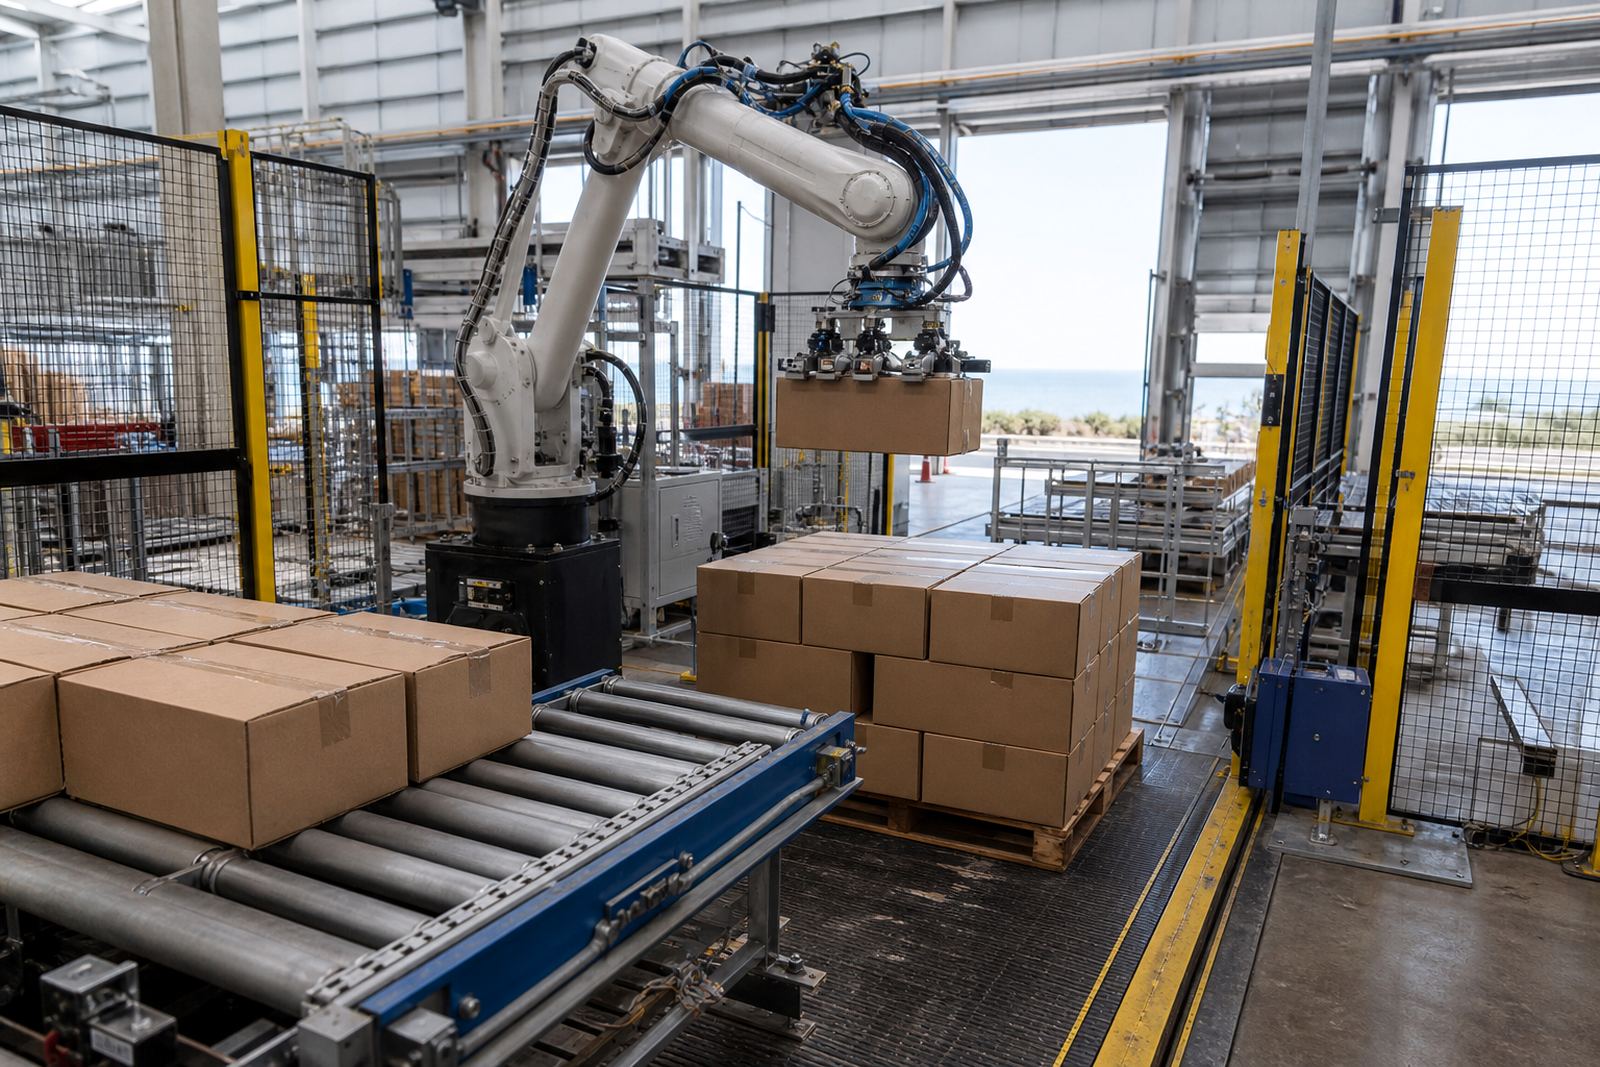
We supplied a retrofit package built around a robot for palletising, a packing interface on the conveyor side, and controls integration to tie the new equipment into the existing line. The aim was not to replace everything. It was to add the right automation where it would make the biggest difference and leave the rest of the plant in place.
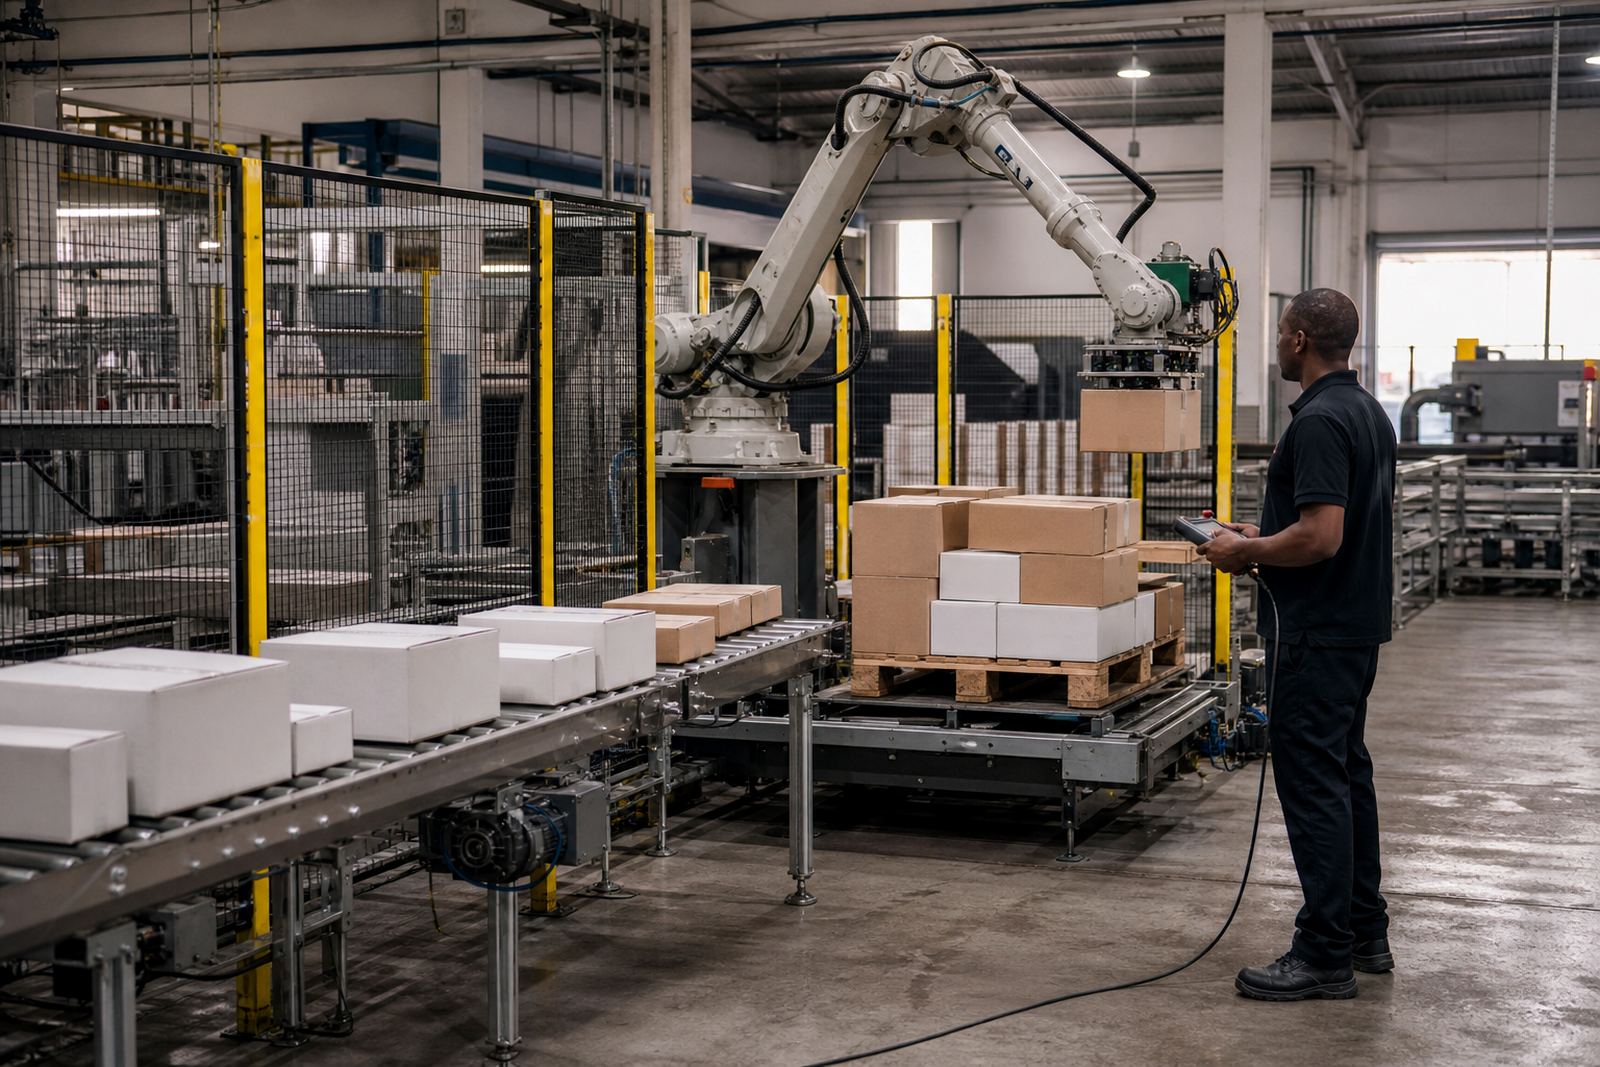
The palletising side was set up to handle multiple patterns, with recipe based selection for different carton footprints and stack heights. The packing section was adjusted so mixed SKU cartons could be presented consistently to the robot side, while keeping enough flexibility for the operators to manage short runs and product swaps. Safety guarding design was included from the start so the layout could be signed off properly and not treated as an afterthought.
- Robot palletising cell with recipe based pattern selection
- Conveyor integration for carton feed and accumulation
- Controls integration with the existing line logic
- Safety guarding, interlocks and access gates
- Commissioning support for live line start-up
Installation In A Working Factory
The project ran over six weeks from survey to commissioning support, with the mechanical and control work planned around production windows. Spartan based support meant the team could handle site needs in Midrand and keep the shutdown periods tight. We staged the install so the client could continue limited production while sections of the line were upgraded, which reduced disruption and kept stock moving.
During installation, we aligned the new equipment to the existing conveyors, checked transfer levels and tested carton flow under different load conditions. There were a few small adjustments on the day, as is normal on a retrofit, mostly around sensor placement and carton guide settings. The final handover included operator training, fault response routines and the basics of safe daily start up.
- Timeline: 6 weeks end to end
- Commissioning carried out on site after mechanical completion
- Operator training included changeover steps and safe access rules
- Maintenance support notes issued for routine checks and wear points
Results On The Floor After Changeover
Once the line was running, the main benefit was flexibility. The client could switch between pallet patterns without reworking the whole area, and the packing side handled the mixed carton sizes more consistently. Operators were no longer doing as much manual lifting at the pallet build point, which eased strain on the shift and reduced the stop start rhythm that used to slow the line down.
The site also gained a cleaner maintenance and fault finding setup. With the guarding positioned properly and the controls integrated into the existing process, it became easier for the team to see where problems were coming from and respond before small issues spread through the line. Throughput was steadier, and the pallet output was more predictable across mixed runs. Not perfect every day, but far better than the old setup.
- More flexible pallet pattern changes
- Less manual handling at the pallet build point
- More consistent carton presentation to the robot side
- Clearer fault finding and maintenance access
What We Would Rework On The Next Mixed SKU Site
If we were doing the same type of retrofit again, we would keep the same order of work: survey first, then layout, then controls, then guarding and commissioning. That sequence matters on mixed SKU sites because the process only works well when the robot, conveyors and safety measures are planned together rather than bolted on in pieces.
We would also repeat the detailed attention to changeovers. On this kind of line, the smaller practical details matter, such as carton guides, sensor positions, access for cleaning and the speed of recipe selection. In a South African factory, where power interruptions and shift pressure are part of daily life, a retrofit has to be simple to run and easy to recover after a stoppage. That is the difference between automation that helps and automation that becomes another headache.
- Keep the survey and risk work upfront
- Design for frequent changeovers from day one
- Allow for recovery and restart routines
- Build in maintenance access for real day to day use
Key facts
| Project location | Midrand, Gauteng |
|---|---|
| Site type | Manufacturing line with mixed carton sizes |
| Scope | Packing retrofit, robot palletising, conveyor integration, controls integration |
| Safety scope | Guarding design, access control, risk assessment support |
| Timeline | 6 weeks |
| Base team | Spartan, Kempton Park |